Fire Pump Supplier in Indore, Madhya Pradesh – Runfire & Security Systems | All Types of Fire Pumps Available Across India
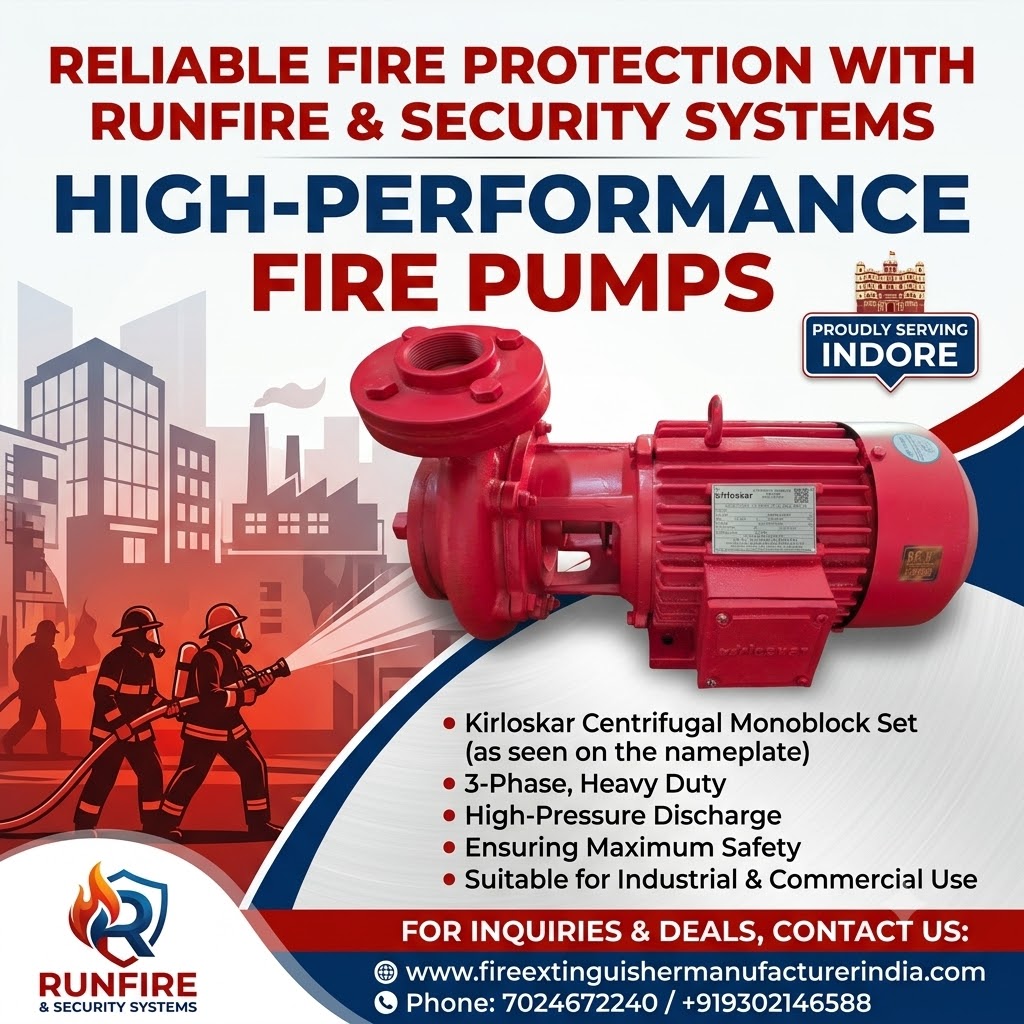
Looking for a reliable fire pump supplier in Indore, Madhya Pradesh? Runfire & Security Systems offers a range of fire pumps for fire hydrant systems, automatic sprinkler systems, industrial fire protection, commercial buildings, warehouses, factories, hospitals, hotels, and residential projects. We cater to fire safety requirements in Indore and supply fire safety products to customers across India.
Fire pumps are a critical component of fire protection systems, helping deliver the required water flow and pressure to firefighting equipment during emergencies. Selecting the right fire pump is essential for developing an effective fire protection system for your facility.
At Runfire & Security Systems, Indore, we help customers explore fire pump options according to their project requirements, system specifications, and applicable fire safety standards.
What Is a Fire Pump and Why Is It Important?
A fire pump is a specially designed pump used to supply water at the required pressure and flow rate to fire protection systems. It supports firefighting operations by delivering water to hydrants, hose reels, sprinkler networks, and other connected firefighting equipment.
Fire pumps are commonly installed in industrial plants, manufacturing units, commercial complexes, shopping malls, hotels, hospitals, educational institutions, logistics centres, and residential buildings.
A properly selected fire pump can help ensure that the fire protection system receives an adequate water supply when required. Pump selection should consider the building's fire protection design, hydraulic calculations, water availability, and applicable standards.
Types of Fire Pumps Available at Runfire & Security Systems
Runfire & Security Systems caters to different fire pump requirements for industrial, commercial, and residential fire protection projects.
1. Electric Motor Driven Fire Pump
An electric motor driven fire pump uses an electric motor to operate the pump and deliver water to the fire protection network.
Key features and applications:
Suitable for compatible fire hydrant and sprinkler systems.
Used in commercial buildings and industrial facilities.
Supports the required water flow and pressure when correctly selected.
Can be integrated with an appropriate fire pump control panel.
Available in configurations selected according to project requirements.
Electric fire pumps are commonly considered for buildings where a suitable and reliable electrical supply is available.
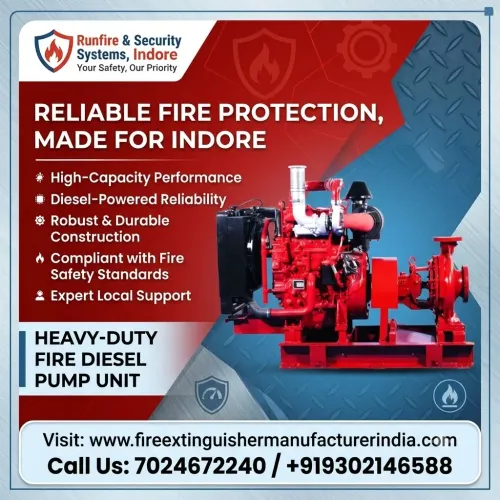
2. Diesel Engine Driven Fire Pump
A diesel engine driven fire pump operates using a diesel engine rather than relying on an electric motor as its primary driver.
Key features and applications:
Suitable for fire protection systems requiring an engine-driven pump.
Commonly considered for industrial plants, factories, warehouses, and large commercial facilities.
Can provide an alternative pumping arrangement when electrical supply reliability is a concern.
Requires suitable fuel storage, ventilation, exhaust arrangements, and maintenance.
Should be selected according to the approved fire protection system design.
Diesel fire pumps are often incorporated into fire pump installations alongside electric pumps, depending on the project's design and applicable requirements.
3. Jockey Pump for Fire Fighting Systems
A jockey pump, also known as a pressure-maintenance pump, helps maintain the required pressure in a fire protection pipeline.
Unlike the main fire pump, a jockey pump is generally designed to compensate for minor pressure losses and small leaks in the system.
Benefits of a jockey pump:
Helps maintain pressure in the fire protection network.
Reduces unnecessary starting of the main fire pump due to minor pressure drops.
Supports automatic pressure maintenance when properly configured.
Commonly used with fire hydrant and sprinkler installations.
The jockey pump capacity and pressure settings should be coordinated with the main fire pump and the overall system design.
4. Horizontal Split Case Fire Pump
Horizontal split case fire pumps are used in applications requiring substantial water flow and dependable performance.
These pumps are commonly considered for large industrial facilities, manufacturing plants, warehouses, commercial complexes, and major fire hydrant installations.
Typical advantages:
Suitable for high-flow fire protection applications.
Designed to facilitate maintenance access, depending on the model.
Available in different capacities and pressure ratings.
Can be selected for large fire hydrant and sprinkler networks.
The final selection depends on the required duty point, installation conditions, water supply, and manufacturer's specifications.
5. End Suction Fire Pump
An end suction fire pump is a centrifugal pump configuration in which water enters through the suction end and is discharged through the outlet.
Keywords